Step 1: monitored while the cable is being made
On the Komax Gamma 450 fully automatic cable processing machine, crimp force monitoring records the force curve of every crimp and detects deviations such as missing strands. Cut-in monitoring reports when a blade touches the conductor during stripping. Cameras check the stripping and the seating of the seals; faulty cables are cut up and removed from the process.
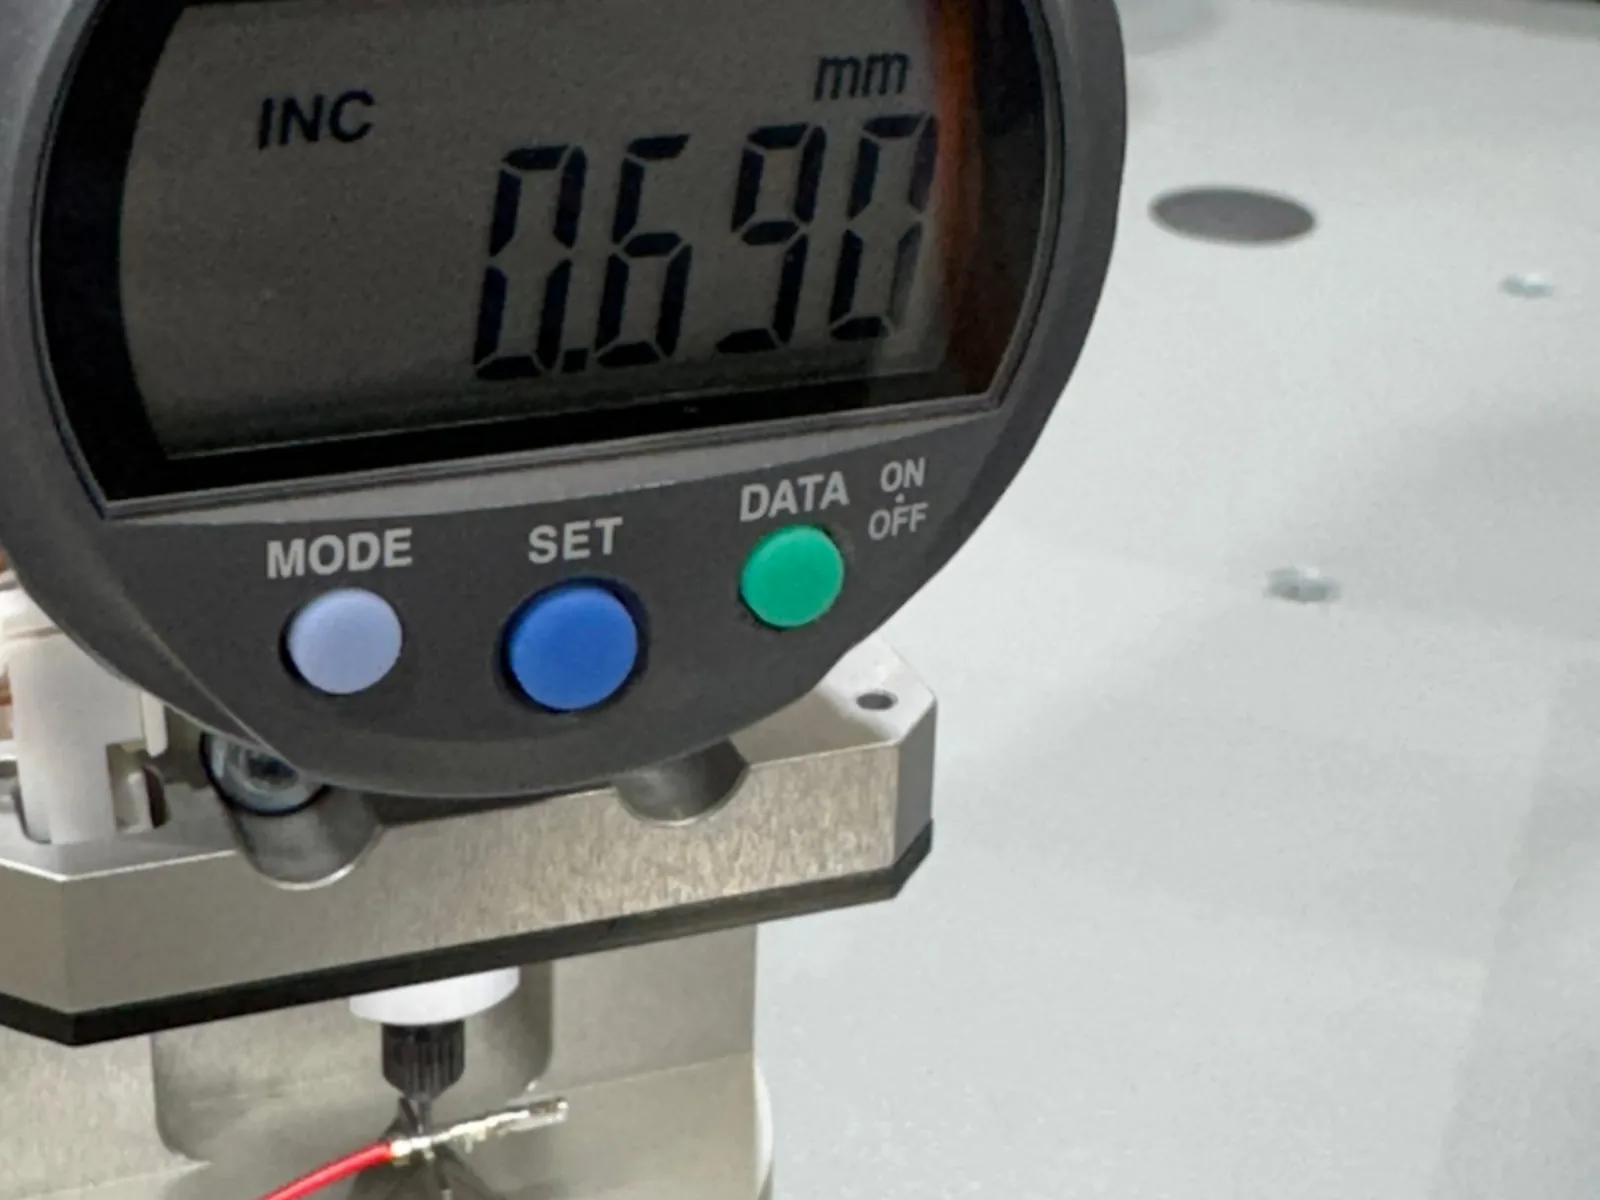
Before an order starts, the crimp height is measured with the Komax 341 measuring device. If it deviates from the target value, production does not begin.
Step 2: final testing on the finished wiring harness
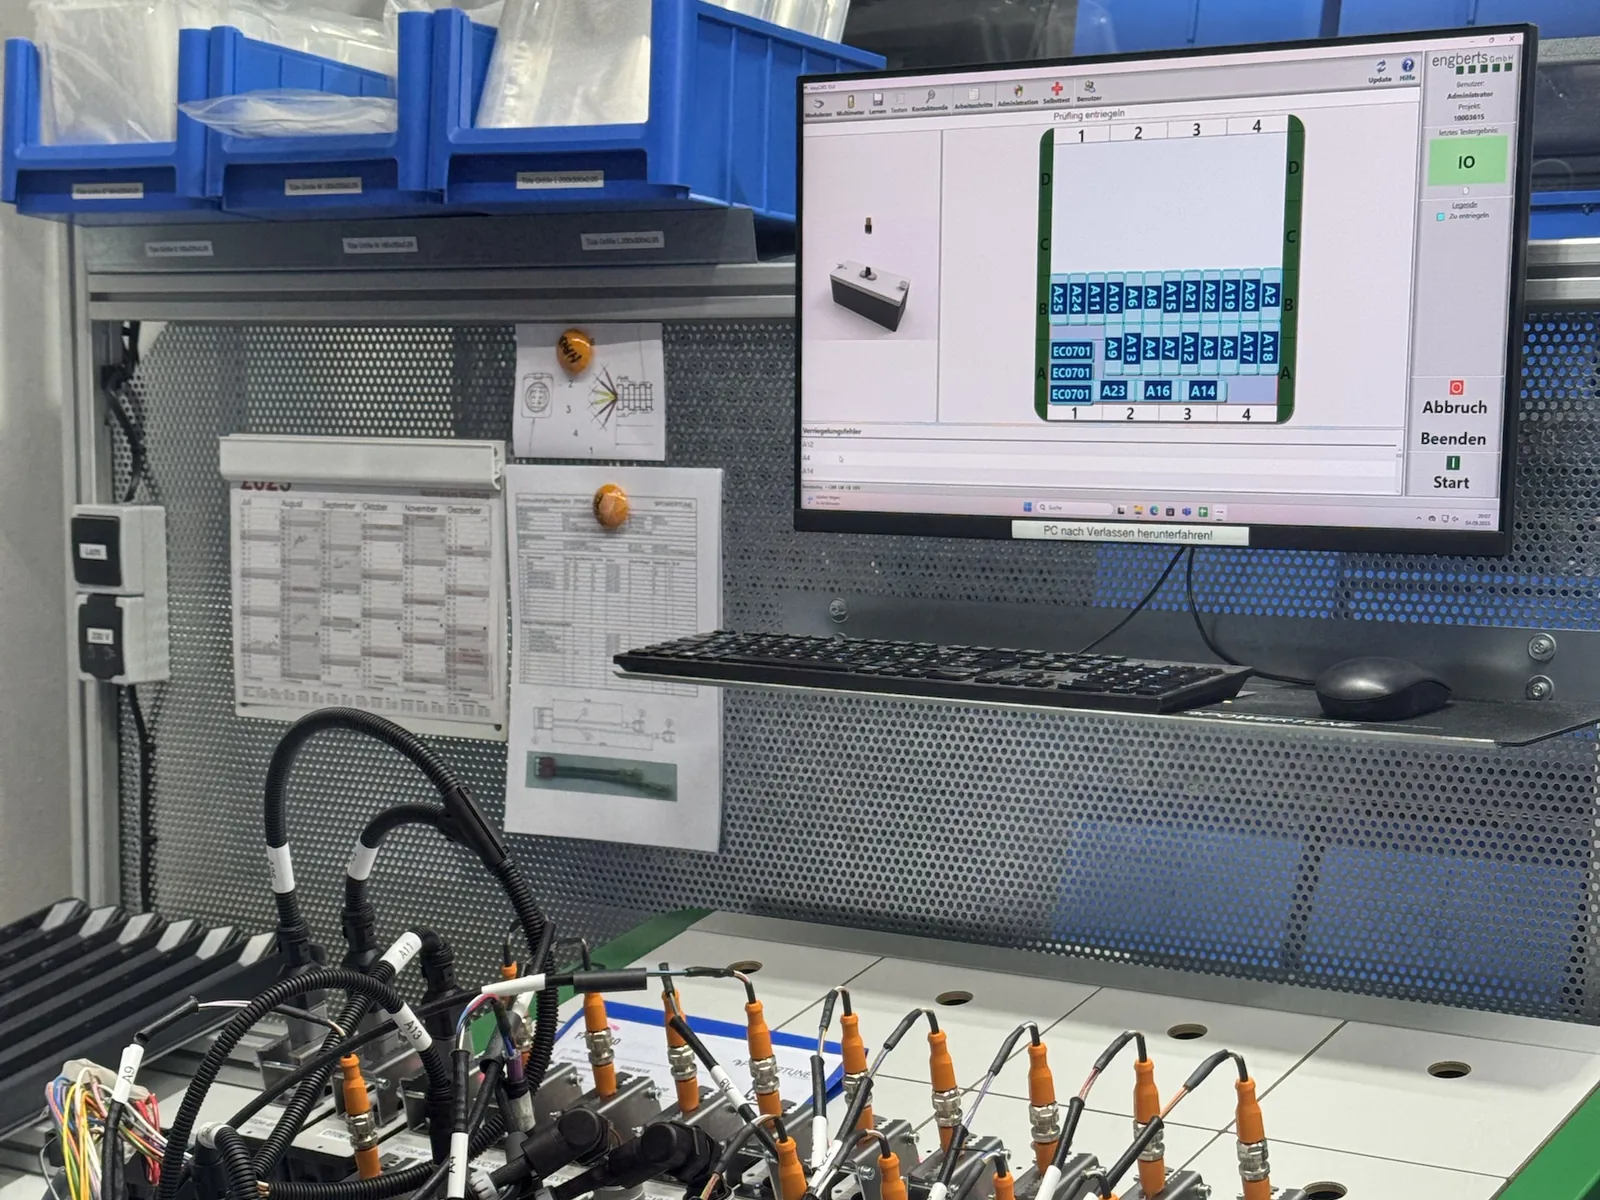
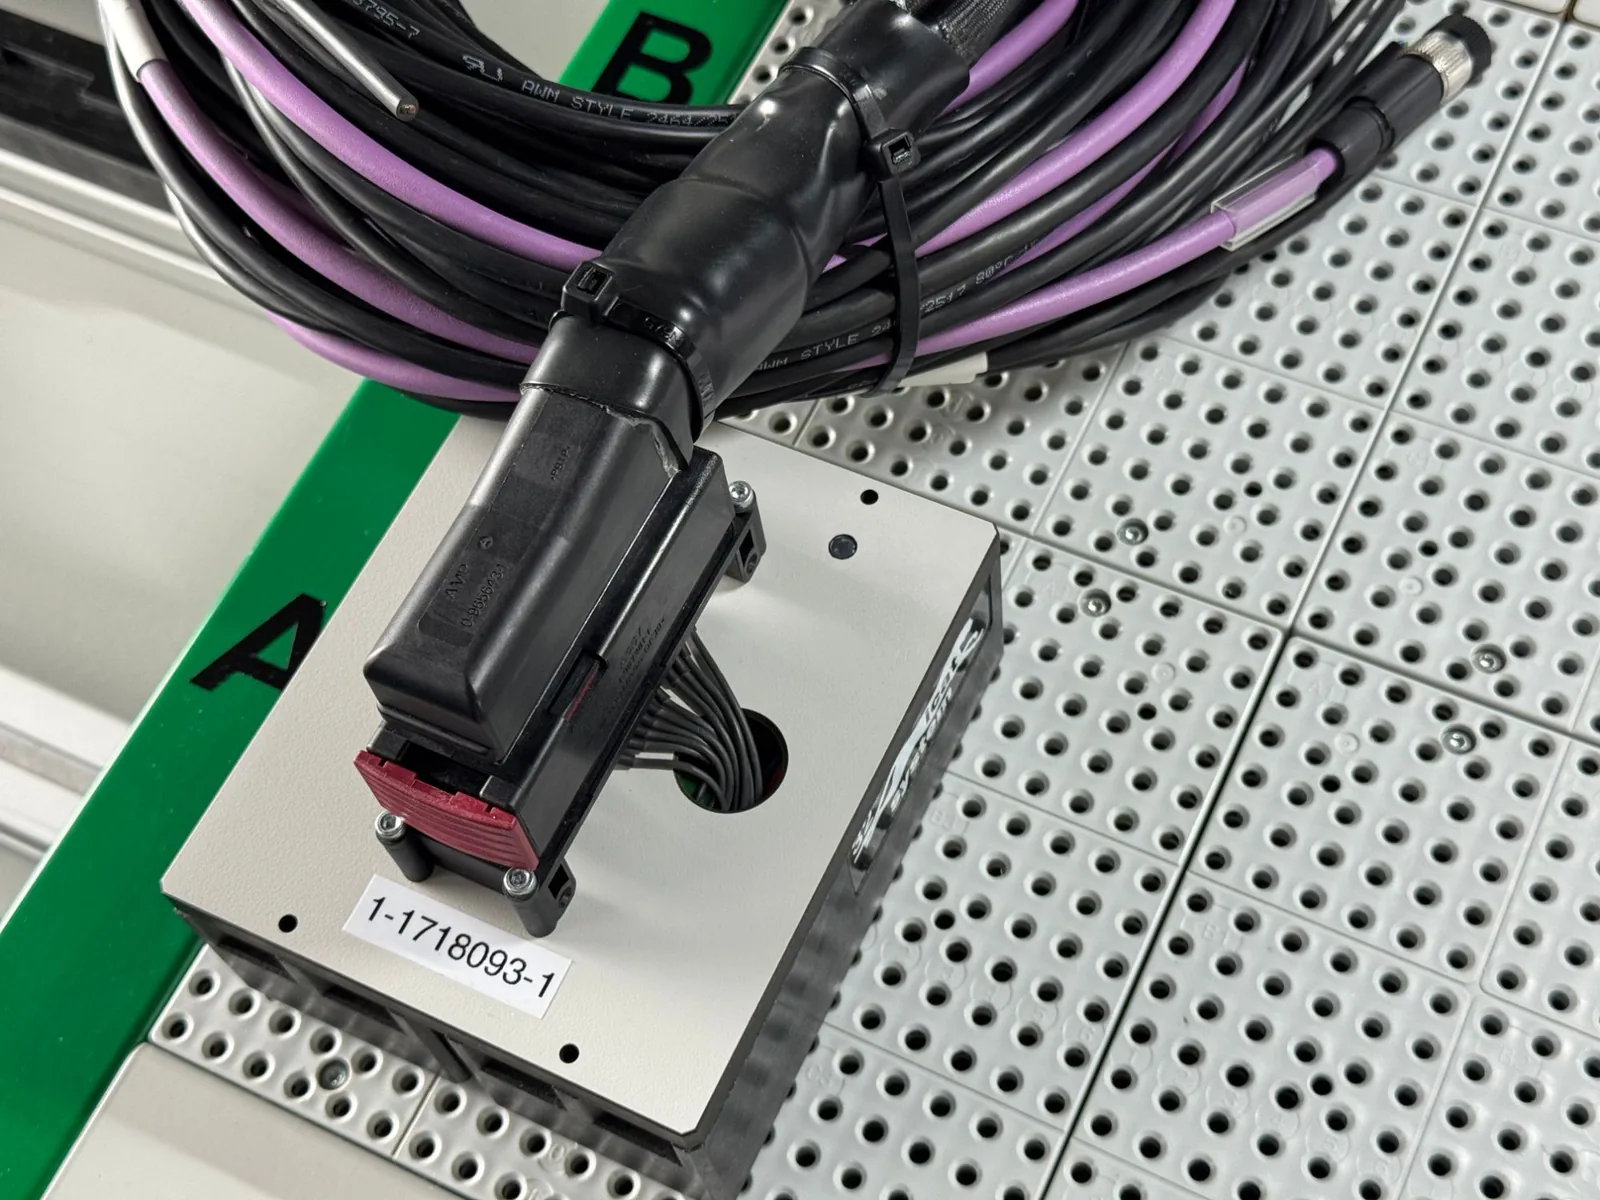
The electrical final test runs on two test systems from Engberts (iCAT). For every connector there is a matching test module with the mating connector, marked with its own number and DataMatrix code. The wiring harness is plugged in connector by connector; the test software guides the operator through the sequence and shows the result directly at the workstation.
We test wiring harnesses with open cable ends on test boards: every end is labelled and contacted via a terminal.
- Pin assignment: does every cable arrive at the correct contact?
- Continuity: are there any interruptions?
- Short circuit: are cables connected that have to stay separate?
- Further tests such as high voltage or function, depending on the requirements
Step 3: records and traceability
On request we prepare test records with every delivery. Our MES makes every delivery traceable down to the individual cable, from the material used to the finished wiring harness.
You can read more under Testing & documentation and in the article Testing wiring harnesses.